ITERATION PLAYBOOK

Rapid injection molding factory path before steel

For a startup bridging 200 pieces, compare CNC, SLA, SLS, MJF, a 3D-printed tool and an aluminum tool against the same drawing before you accept a substitute. This page is a purchase-decision checklist, not an ESG statement, carbon claim, or net-zero story.
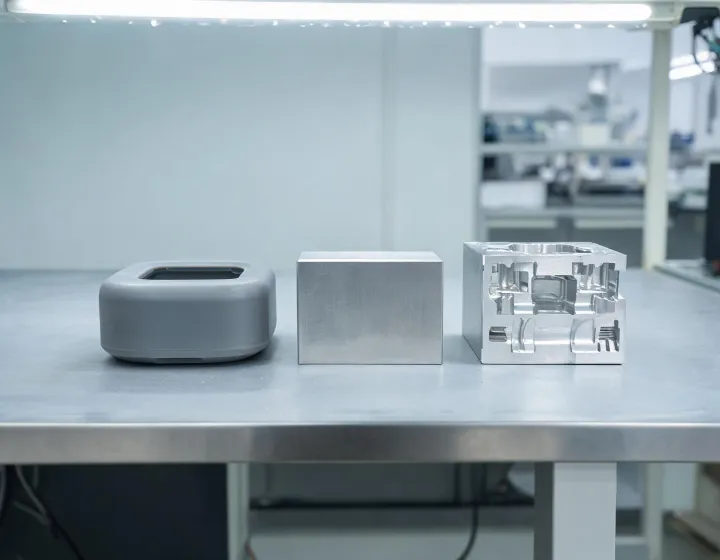
SLA print, CNC blank and aluminum mold insert on one bench

Specification choices that remain open on a 200-piece bridge

Files to request on a prototype path

These labels are buyer reminders, not badges this desk holds.

What to verify before accepting an alternative

CNC versus additive parts

CNC advocates cite production-grade materials and true mechanical properties. Additive-part advocates cite 24–48 hour loops and geometry that milling cannot reach. Those routes do not replace a 200-piece molded lot. If you accept MJF in place of molded ABS, write which tests are waived. If you accept CNC in place of a first tool, write which gate and knit-line risks remain untested.

Aluminum tool versus 3D-printed tool

Printed-tool advocates cite lower NRE and a faster first cavity while revision C is still moving. Aluminum-tool advocates cite a stabler shrink map, SPI texture, and a shot-life that more often covers 200 pieces in one cavity. Accepting either route as “good enough for launch” without a shot-count limit written on the quote is how a bridge insert becomes an unplanned reprint or an unplanned steel PO.

RouteTypical buyer checkLimitation to disclose
SLACosmetic envelope, clip fitUV aging and production resin mismatch
SLS / MJFLiving hinge screening, ductsSurface roughness versus SPI texture
CNCSnap fit in production polymerNo gate, no knit line, no mold shrink map
Printed toolFast first cavity, ECO-friendly insertShot-count often below 200 unless written
Aluminum toolT1 molded parts, gate vestigeShot-life and steel-upgrade trigger

Inspection method stays explicit: optical scan, CMM, or caliper-only. Build volume and layer resolution matter for additive parts; shot weight, clamp tonnage and the shot-count limit matter once a press is in the packet. None of those numbers are guaranteed by this desk.

Lock the 200-piece choices, then request quotes

State which process is required, whether an aluminum tool or a printed tool is allowed, quantity, destination and the first inspection pack. Optional budget and preference merge at submit time.

Enter a contact name.
Enter a work email.

Include specifications, quantity, destination and delivery timing. No existing quotation is required to start. After contact, send STEP/PDF drawings by the reply channel we confirm.